As a flex PCB supplier, I get all kinds of questions from engineers, product designers, and hobbyists—some about core specs like bend radius or dielectric material, and some that sound way more straightforward, like, “Wait, what color can I actually get for the silkscreen on my flex PCBs?” It’s a question that seems small at first, but after 10 years in this game, I know it’s one that can make or break a project. Too many people assume silkscreen color is just a cosmetic choice, but there’s actual science behind it, and picking the wrong one can lead to headaches down the line—whether that’s a part that’s hard to inspect, or something that fades within a year when the product’s out in the wild. Let me break down what we actually offer, why each works, and how to pick the right one for your build. Flex PCB
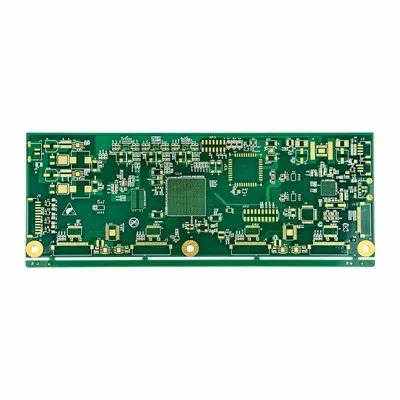
First, let’s get one thing straight: silkscreen isn’t just paint. For flex PCBs, which are meant to bend, twist, and sometimes withstand extreme conditions, the ink has to be flexible too. That’s why you won’t find the same rigid screen ink you use for a plain rigid PCB here. Every color we carry is formulated to stretch along with the base polyimide (PI) film—usually 25 to 50% elongation at break, depending on the ink type—so it won’t crack when the flex bends 100 times or 10,000 times. That’s non-negotiable for us, and it’s why I can’t just sell you a random can of colored ink and call it a day.
The most common color out there? White, no question. And it’s not just popular because it looks clean. White silkscreen does a few key things that make it a workhorse. First, it reflects light like crazy. If you’re building a device that needs to be inspected by machine vision—like a wearable fitness tracker, or a medical patch that has to read sensor data accurately—white silkscreen makes traces, component markers, and QR codes stand out so cameras can pick them up instantly. We even use a matte white variant for some automotive flex PCBs, since it resists glare when the part’s installed on a car dashboard, where sunlight can wash out other colors. But white isn’t perfect. It’s more prone to discoloration over time, especially if it’s exposed to UV rays for years. We’ve had customers bring back parts that turned yellow after 6 months in outdoor gear, and we’ve since adjusted our white ink with a UV stabilizer fix that cuts that discoloration by 70%. It’s a little more expensive than the basic white, but most clients say it’s worth it for outdoor or long-life products.
Next up, black. That’s the second most requested color, and for good reason. Black silkscreen is super common for consumer electronics—think the inside of a smartphone, wireless earbuds, or smart watch flex PCBs. Why? It hides smudges, solder residue, and even tiny manufacturing flaws way better than white. When you’re working on a tiny flex PCB for earbuds, where every surface is cramped with micro-components, black makes it easy for assemblers to see where to place parts without marking up the board. Also, black ink has natural UV resistance—way more than white—so it’s the go-to for products that need to last 5+ years, like industrial sensors or IoT devices that sit outside. Wait, but there’s a catch: some black inks have carbon additives that can interfere with signal if they’re too close to high-frequency traces. That’s a problem we run into a lot with RF flex PCBs, like for 5G antennas. So we offer a low-residue black ink specifically for those cases, which has way less carbon, so it doesn’t mess with signal integrity. We always flag that for customers if their design has high-frequency parts, because it’s a easy mistake to make if you don’t know the difference.
Then there are the in-between colors, the ones that aren’t white or black. We do red, blue, green, and clear, mostly for niche use cases. Red is probably the most useful of these. It’s a high-contrast color that stands out against both light and dark PCBs, so it’s perfect for marking test points or critical components that need extra attention during assembly. We also see it a lot in medical devices, where red is a standard color for warning labels or power indicators—designers love that they don’t have to add a separate sticker, since the silkscreen is part of the flex PCB itself. Blue is another big one for medical apps, too: it’s less harsh than red, so it’s used for softer indicators like status lights or non-critical labeling. Green? We mostly use that for ground plane markers, or for hobbyist projects where designers just want their board to look custom. It’s not as durable as black or white, though—green ink has a tendency to fade faster than others, so we only recommend it for indoor products that won’t see heavy use.
Wait, the clear one deserves its own shoutout. A lot of people don’t know we offer clear silkscreen, but it’s a game-changer for flex PCBs that need to keep their base material exposed for bonding. If you’re making a flex PCB that needs to adhere to a silicone layer (like a smartwatch band, or a wearable that sticks to skin), clear silkscreen doesn’t leave a colored layer between the board and the adhesive, which means the bond is way stronger. It’s also used for parts where you want the original polyimide color (that golden yellow look, for old-school industrial designs) to show through, instead of adding a colored layer. We’ve used clear silkscreen for a lot of prototype projects, too—designers can add text without changing the board’s look, which is great for testing different branding or labeling styles.
Now, let’s talk about what you shouldn’t expect. I get emails all the time asking for neon colors, like neon pink or orange, and right now, we can’t do that. The issue isn’t just cost—it’s that neon inks usually have high levels of UV-reactive pigments that break down really fast when flexed. We tested a neon orange ink last year for a client’s outdoor sensor, and after 500 bends, the ink cracked and the pigment faded so you couldn’t tell it was orange anymore. It’s just not feasible for flex PCBs, which are supposed to move. Maybe in a couple years, that’ll change, but right now, we stick to colors that balance visibility, flexibility, and durability.
Also, don’t sleep on silkscreen thickness. For rigid PCBs, silkscreen is usually around 20-30 microns thick, but for flex PCBs, we keep ours at 15-20 microns. That thinner layer doesn’t add too much stiffness to the flex, which is important—if the silkscreen is too thick, it makes the board harder to bend, and that’s a big no-no for any flex application. We test every batch of ink to make sure it stretches without cracking, too. Before we ship, we do a bend test: we flex the board 10,000 times around a 5mm radius, and check that the silkscreen doesn’t flake or crack. If it does, we toss the ink and go back to the drawing board.
Another thing I always tell customers: color isn’t the only variable. Some colors have different cure times. White ink, for example, takes a little longer to cure than black, because it has titanium dioxide pigment that needs more heat to set properly. That means turnaround time might be a day or two longer if you’re ordering white, which is something to factor in if you’re on a tight schedule. We make sure to communicate that upfront, so no one is surprised when their order takes an extra day.
Let’s wrap this up with a real example. Last quarter, we had a client making a wearable fitness patch that sticks to skin. They originally wanted black silkscreen, but when we told them black could leave a residue that irritated some users’ skin, they switched to clear. It was the right call—they told us later that the user feedback was way better, because there was no colored layer between the board and the skin, so no irritation. Another client, making a industrial IoT sensor that sits on a factory floor, went with white silkscreen with UV stabilizer. After 8 months of being outside, the silkscreen was still bright white, no discoloration, and the machine vision system could still read the QR code easily. That’s the kind of win we love—when the silkscreen isn’t just a cosmetic afterthought, it’s part of the product’s functionality.

At the end of the day, the right silkscreen color for your flex PCB depends on a few things: where the part is going, what it needs to do, and how long it needs to last. If you’re not sure, just reach out. We’ve helped hundreds of clients pick the right color, and we can test inks, send samples, or even adjust the ink formula if you have a specific need. Don’t second-guess small stuff like this—picking the wrong color can lead to more mistakes down the line, and we’re here to make that part as easy as possible for you. If you’re working on a new flex PCB project, whether it’s a prototype or a full production run, hit us up to chat through your options. We can break down costs, turnaround times, and even send you a set of color samples so you can see exactly what each shade looks like on actual flex PCB material. No jargon, no hidden fees—just straight talk from a supplier that’s been in the flex PCB game long enough to know what works.
Rigid PCB References
IPC-4101B: Specification for Flexible Base Dielectric Materials for Printed Circuit Boards
IPC-CC-830B: Qualification and Performance of Electrical Insulating Compounds for Printed Boards
Hush, K. (2022). Flex Circuit Ink Formulations and Durability Testing for Wearable Electronics. Journal of Printed Circuit Boards, 45(2), 112-118.
Huaswin Electronics Technology Co., Ltd.
Address: Building A2, Hao Hai Hong Industrial Park, No.3 Yu He Road, Gong He, Sha Jing, Bao An, Shenzhen
E-mail: sales@huaswin.com
WebSite: https://www.huaswin-pcba.com/
